Traceability from component lot to serial number
Track SMT and assembly lines as they run, control components down to the individual reel, and trace by serial number for OEM customers.
Common problems
Line stops for feeder changeovers and component shortages
Short stops are rarely logged, and they add up to hours every week.
Partial reels
Once a reel is opened, nobody knows for sure how much is left.
Constant model changeovers
Several models per shift make it hard to see which line will finish its order on time.
Defects found at the end of the line
Solder defects and missing components surface only after several more steps.
Output known only at end of shift
Plan, actual and gap arrive when the shift is already over.
Traceability to the serial number
OEM customers want to know which component lot went into each unit.
Following the flow of the plant
Component warehouse
Receive by lot with labeled reels; issue by work order; stock down to the reel.
SMT
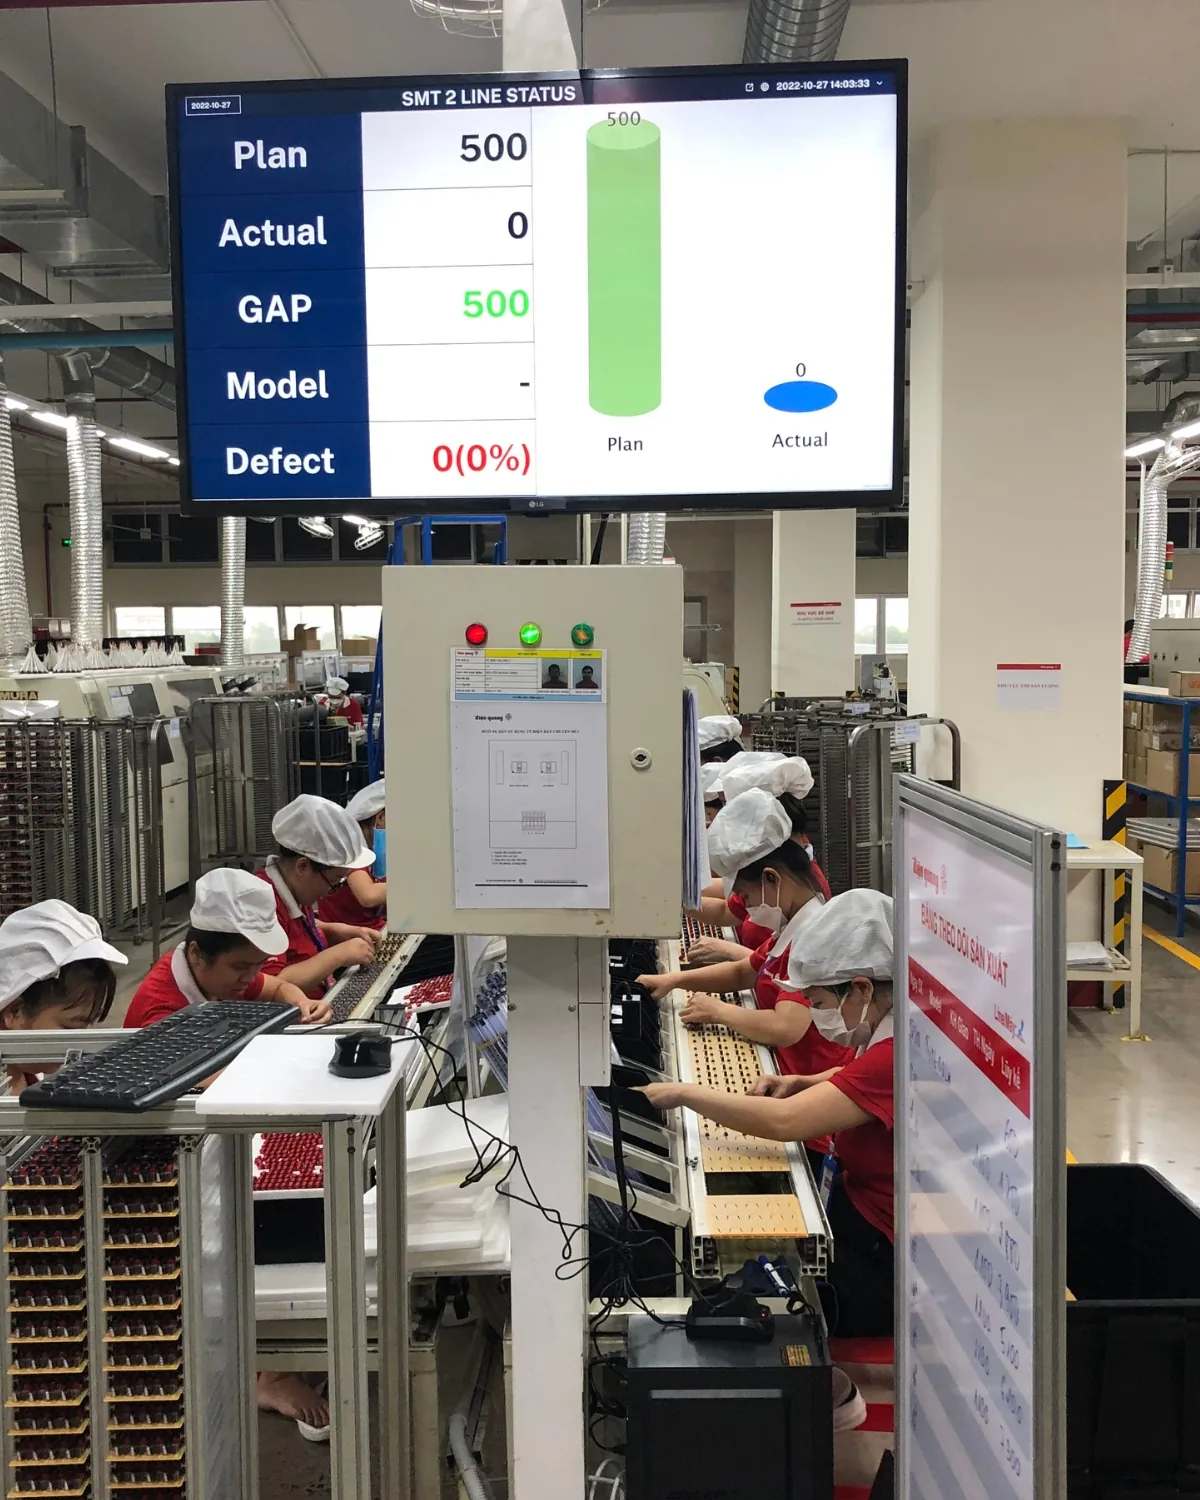
Plan, actual and gap on the line screen; line stops logged by reason.
Post-reflow inspection
Defects logged by code at the inspection station, linked to work order and shift.
Assembly
Progress by work order and model; serial numbers linked to component lots.
Final inspection and packing
Serial numbers scanned at packing, quantity checked per carton.
Finished-goods warehouse
Receive by labeled carton, ship by order; trace back from serial number to component lot.
Modules for electronics
The full set of ControlMES modules is available, configured for electronics. Deploy them one at a time or together, as your factory needs.
| Module | In an electronics plant |
|---|---|
| Master data | Models, component lists, SMT and assembly steps, production standards per line. |
| Planning & scheduling | Plan by model and line; re-sequence when orders change or components run short. |
| Production tracking | Hourly plan, actual and gap on every line's screen. |
| Inventory & material flow | Components by lot and by reel, issued by work order. |
| Quality management | Defects by code at every inspection station; defect rates by line, model and shift. |
| Machine connectivity | Output and run/stop status taken from machines and lines. |
| Traceability | From serial number back to component lot, line, shift and operator. |
| Management reporting | Output, defect rates and at-risk orders across all lines. |
| Maintenance | Planned maintenance for pick-and-place machines and reflow ovens; breakdown history per machine. |
In operation
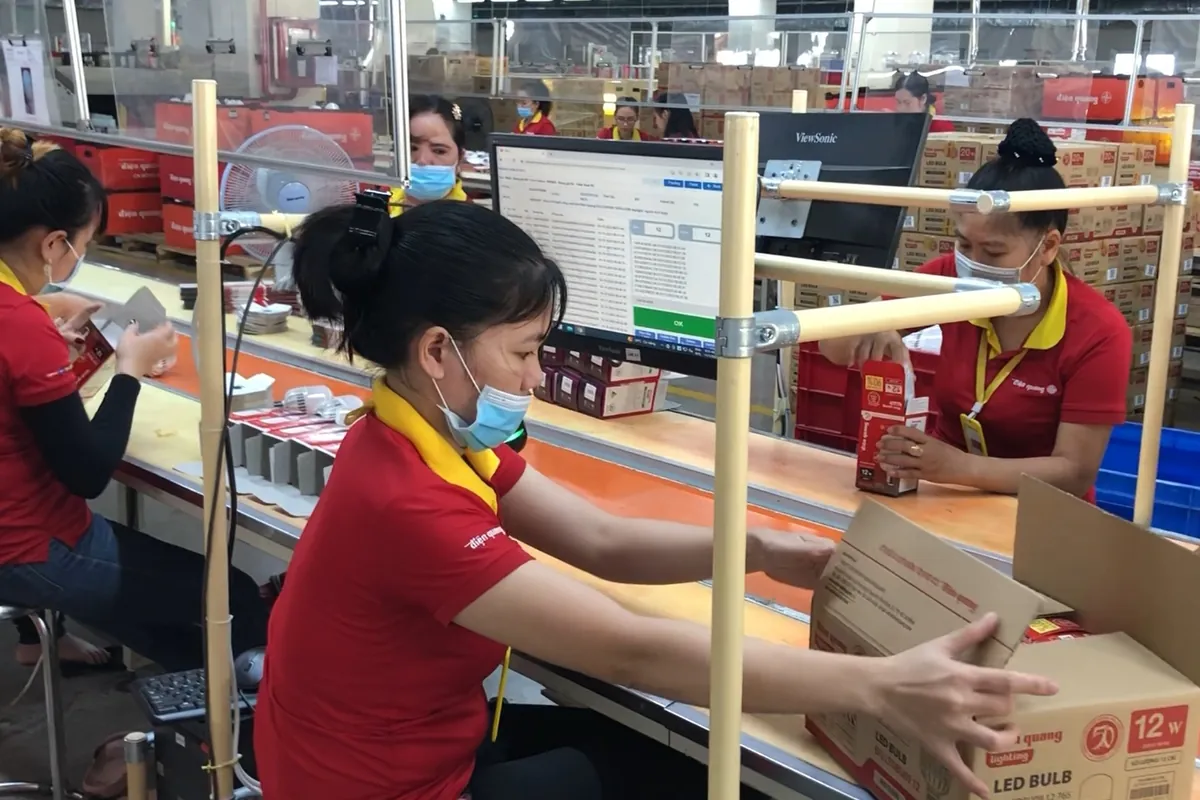
ControlMES is running at an electronics plant, including traceability.
FAQ
Lines stop for feeder changeovers and component shortages, and nobody logs it?
Connected lines record every stop, and the reason is picked on screen at the line. Supervisors see downtime by line and by reason after every shift.
Component stock doesn't match, and nobody knows which reel went to which work order?
Components are managed by lot and by reel, and issued by work order.
An OEM customer asks which component lot went into a serial number, and it takes a whole day to find?
Codes are scanned at component receipt, work order start and packing. From a serial number, trace back to component lot, line and shift in minutes.
Constant model changeovers, and no one knows which line will finish its order on time?
Hourly plan, actual and gap on every line's screen; at-risk orders are flagged early.
Our SMT machines already have their own software.
ControlMES takes output and status data from them without replacing the machine control software.
Contact
A 1-day assessment at your electronics plant, free of charge: we follow one work order from the component warehouse to packing.