From corrugator to finished pallet, know which orders are at risk
ControlMES is fully deployed at a 17-line corrugated packaging plant. Every machine, from the corrugator, printers and die-cutters to the folder-gluers, is connected, and data comes straight from the machines.
Common problems
The corrugator is the bottleneck
One stop affects the entire chain downstream.
Order changeovers eat machine hours
Paper changes, width changes and jams are rarely logged with a cause.
Losses that never reach the report
Paper scrap and trim waste sit outside the output report.
Planning in Excel
With corrugator and print plans in spreadsheets, slipping orders are hard to spot in time.
Defects found too late
Print and die-cut defects are found only after the goods have moved to the next step.
Traceability requirements
FDI customers require traceability from paper lot to box lot.
Following the flow of the plant
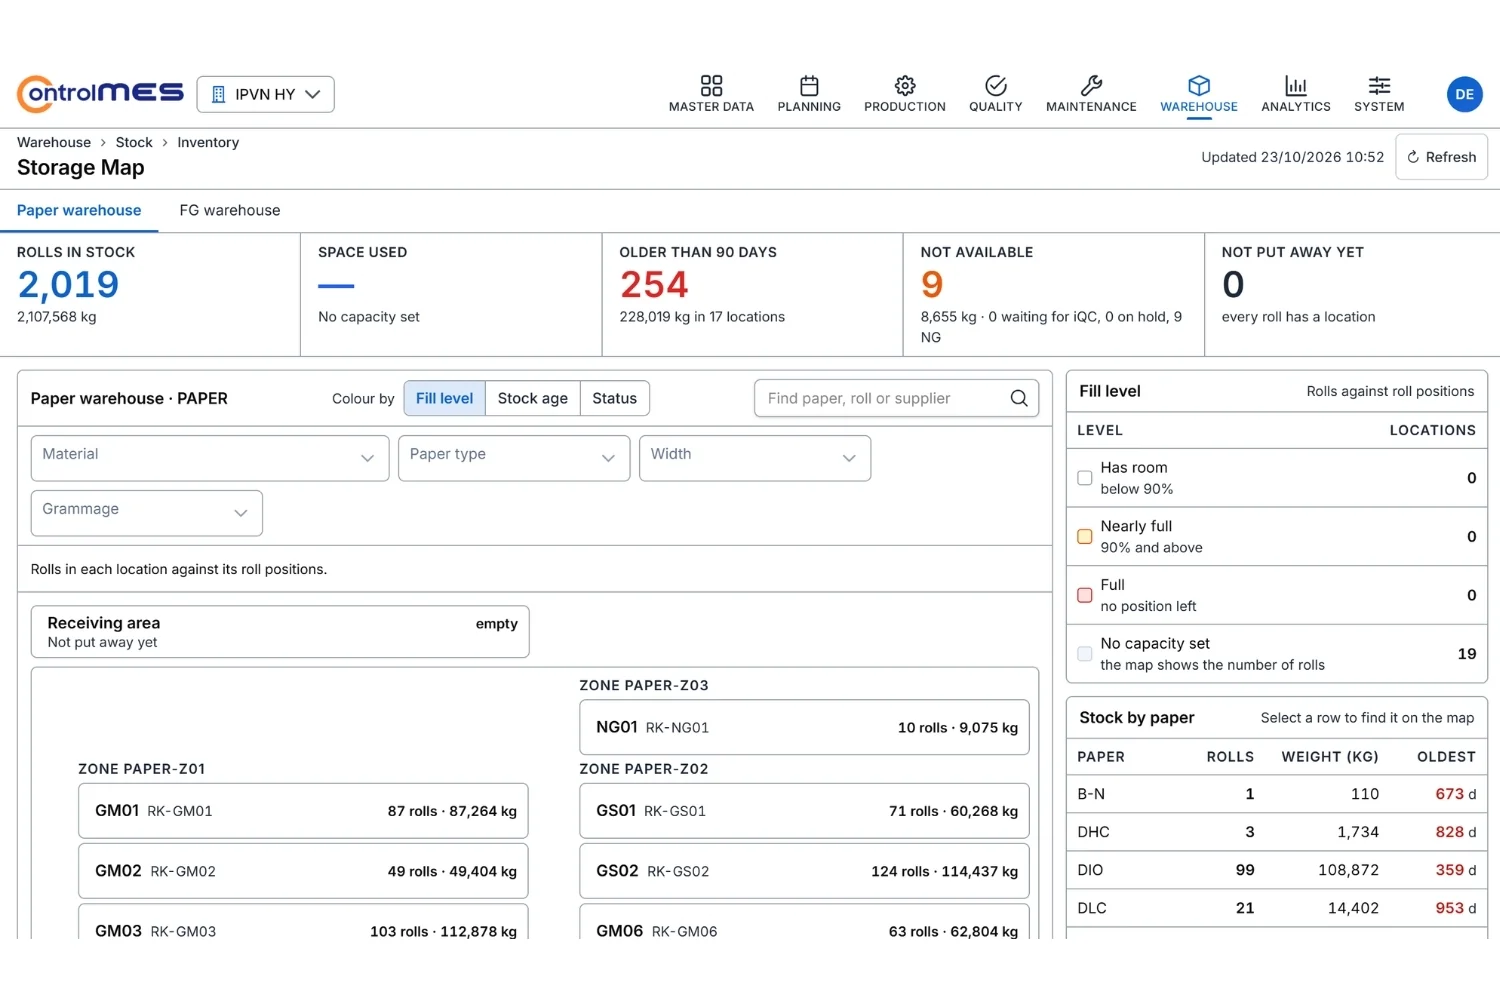
Paper roll warehouse
Receive, inspect and issue paper by work order; stock by individual roll.
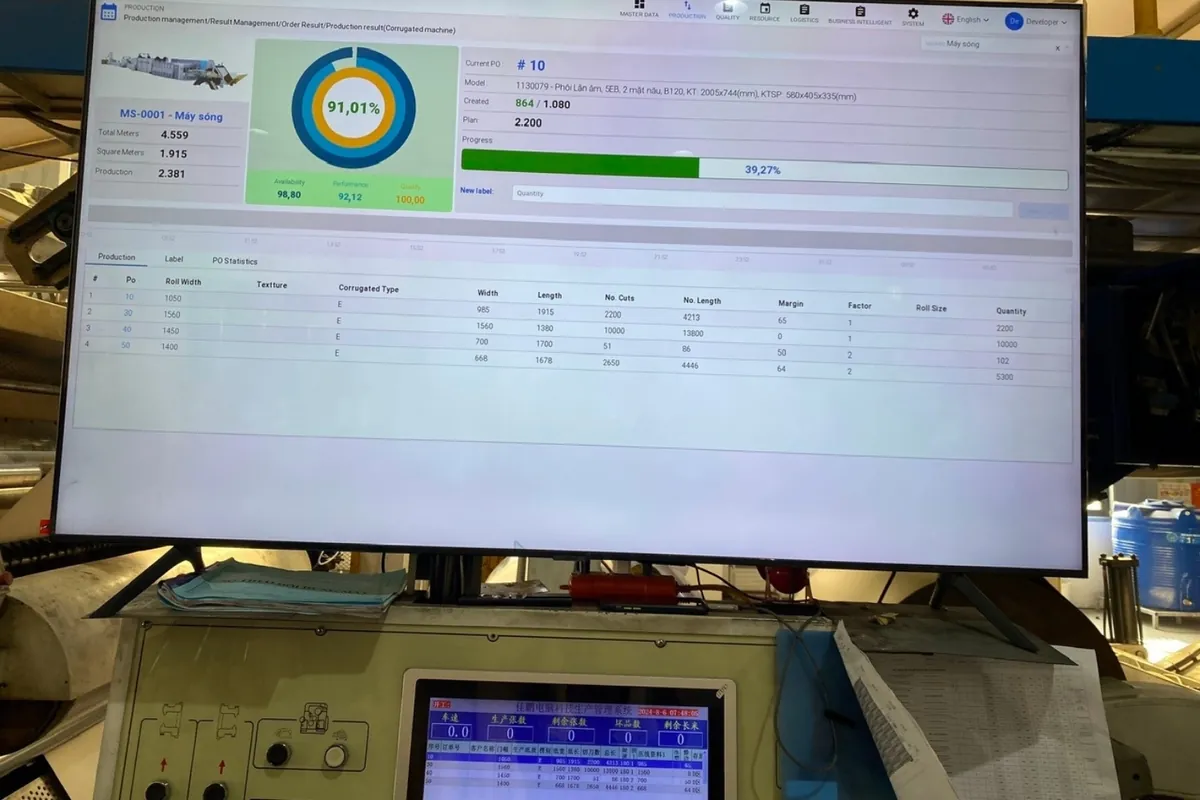
Corrugator
Output, run time and downtime taken directly from the machine; scrap logged by defect code at the dry end.
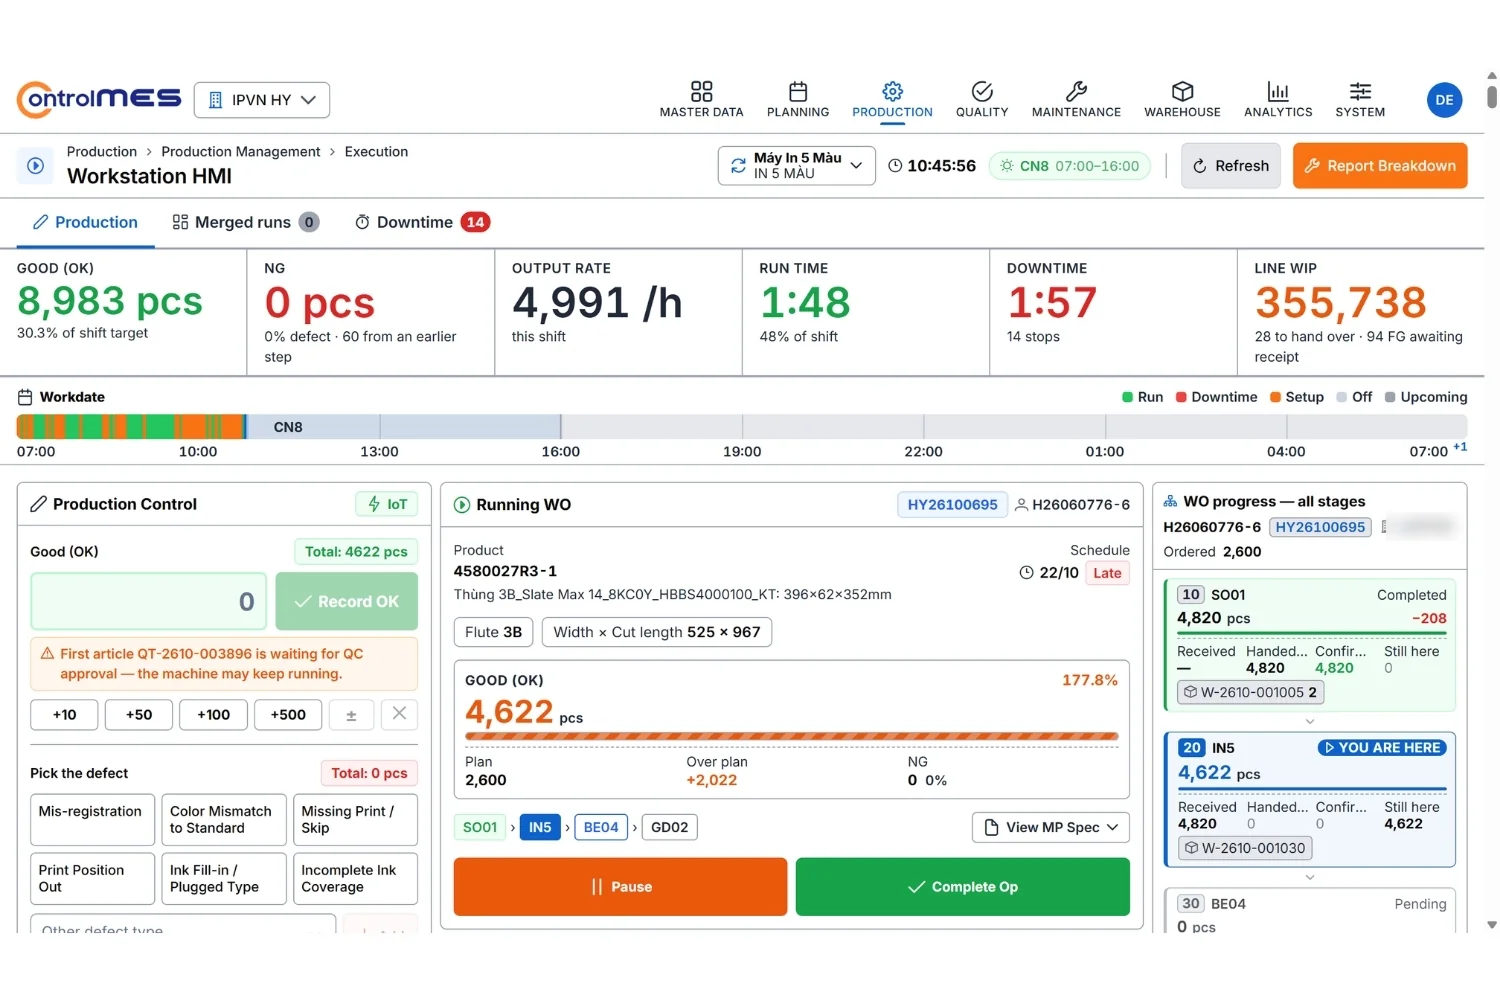
Printing
Output and run/stop status taken from the printer; defects logged by code at the machine, linked to the running work order.
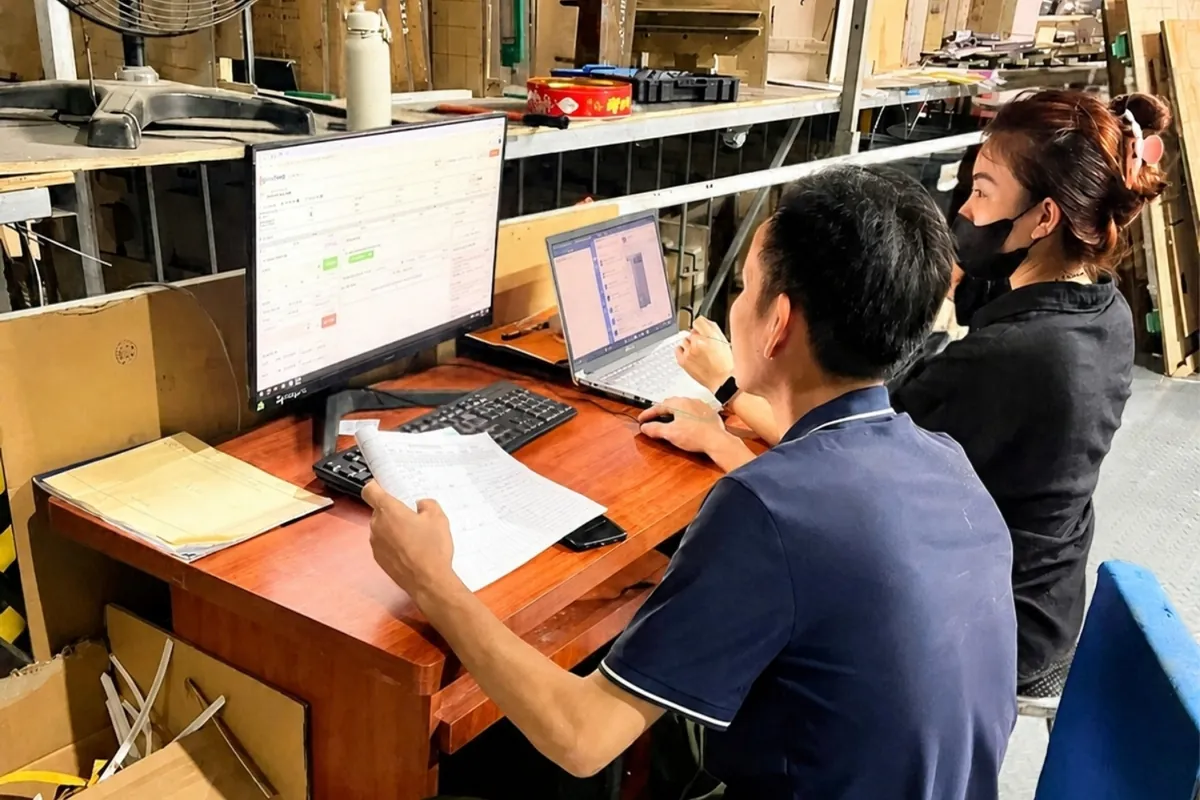
Die-cutting
Output and run/stop status taken from the die-cutter; defects logged by code at the machine.
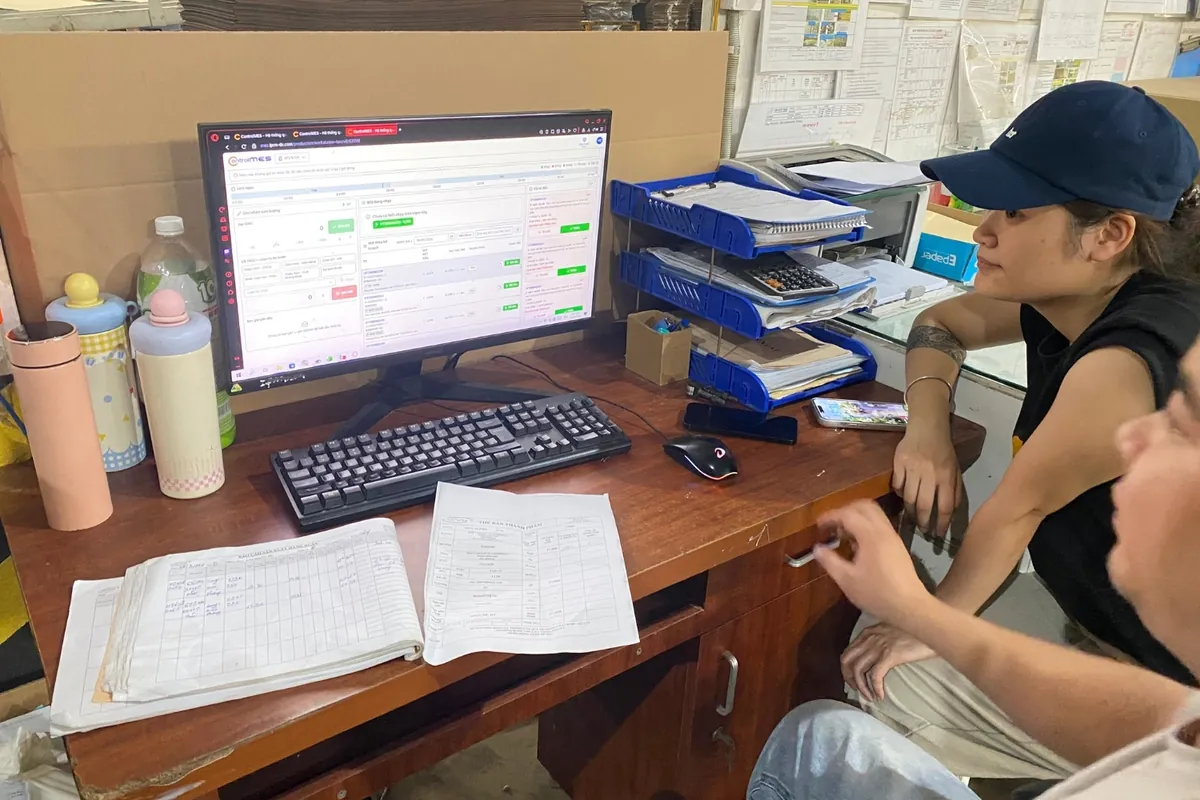
Folder-gluing and finishing
Folder-gluers connected; the finishing area records on screen by work order; you know which orders are ready to ship.
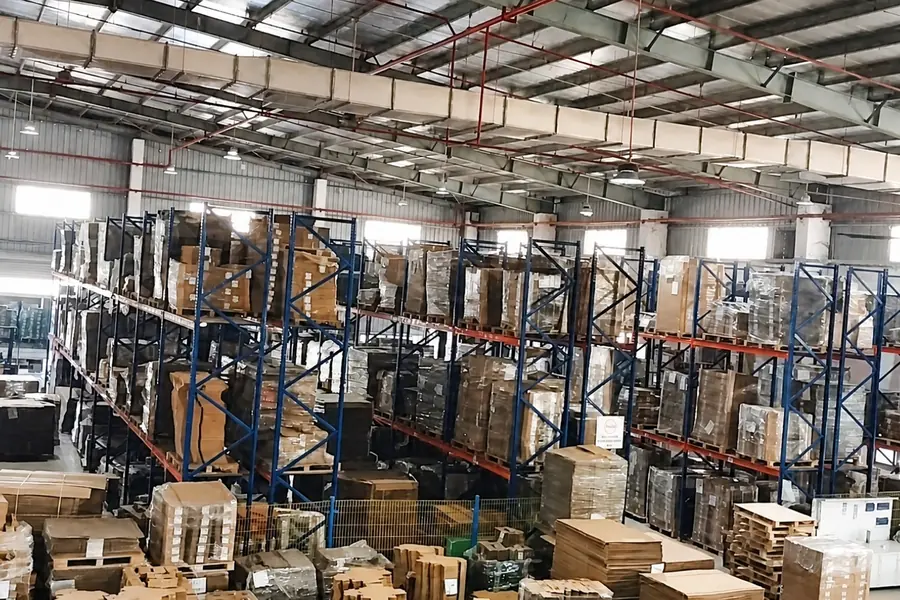
Finished-goods warehouse
Receive by labeled pallet, ship by order, actual stock on hand.
Modules running at the plant
Eight modules in daily use at the 17-line corrugated plant.
| Module | At the packaging plant |
|---|---|
| Master data | Item codes, paper grade per ply, flute type, process steps, production standards, machines, shifts. One trusted source for every department. |
| Planning & scheduling | The production plan for the whole plant is generated automatically in ControlMES from orders and machine capacity. Corrugator orders are combined to reduce trim waste. |
| Production tracking | Every machine connected. Output, run time and downtime by work order and by shift, visible as it happens. |
| Warehouse | Paper rolls tracked one by one: receive, inspect, issue by work order. Finished goods by labeled pallet, shipped by order. A warehouse map shows where everything is. |
| Quality management | Incoming paper inspection and first-piece inspection. Defects logged from each line's own code list; operators pick on screen instead of typing. |
| Maintenance | Planned maintenance, breakdown history for every machine. |
| Analytics & management reporting | The whole plant, its bottlenecks and at-risk orders on one screen. |
| Scrap management | Trim, cores, rejected sheets and damaged paper separated by category and by source. |
A real factory
A 17-line corrugated packaging plant.
Link
Departments check production status in ControlMES instead of walking down to the shop floor to ask.
See
Every machine connected, data taken directly from the machines; the production plan is generated automatically in ControlMES.
Foundation
Item codes, process steps, standards and downtime reasons standardized in 2–4 weeks, with AI assistance.
Lines record production in ControlMES, with every machine connected. When a machine stops, supervisors and management see it on screen immediately, not in the end-of-shift report.
FAQ
Machines stop, nobody logs why, and at month end no one knows where the hours went?
Connected machines record every stop. Operators pick the reason on screen at the machine, and supervisors review downtime by machine and by reason after every shift.
Plans made by hand, and you only find out an order is late once it already is?
The plan is generated automatically from orders and machine capacity. Each work order's progress updates from actual machine output, and at-risk orders are flagged before the due date.
Paper roll stock doesn't match the books?
Paper is tracked roll by roll: received, inspected, issued by work order. The warehouse map shows where each roll is and how long it has been in stock.
No one knows how much paper scrap and trim waste there is?
Scrap is logged by category and by source. Combining corrugator orders cuts trim waste right at the planning stage.
Print and die-cut defects found only at the next step?
First-piece inspection at the machine, defects logged by code the moment they are found, linked to work order, machine and shift.
Can you connect imported machines with no documentation?
Yes. ControlMES reads run/stop and output signals without touching the machine's control system.
Contact
A 1-day assessment at your packaging plant, free of charge: we follow one order from the paper warehouse to finished goods.